Batch vacuum brazing of aero-engine titanium blades
0.5 mm thin-wall TC4 blades, 0.05–0.1 mm gap, 240 parts per charge, 6 months of serial delivery with 99.2% first-pass yield.
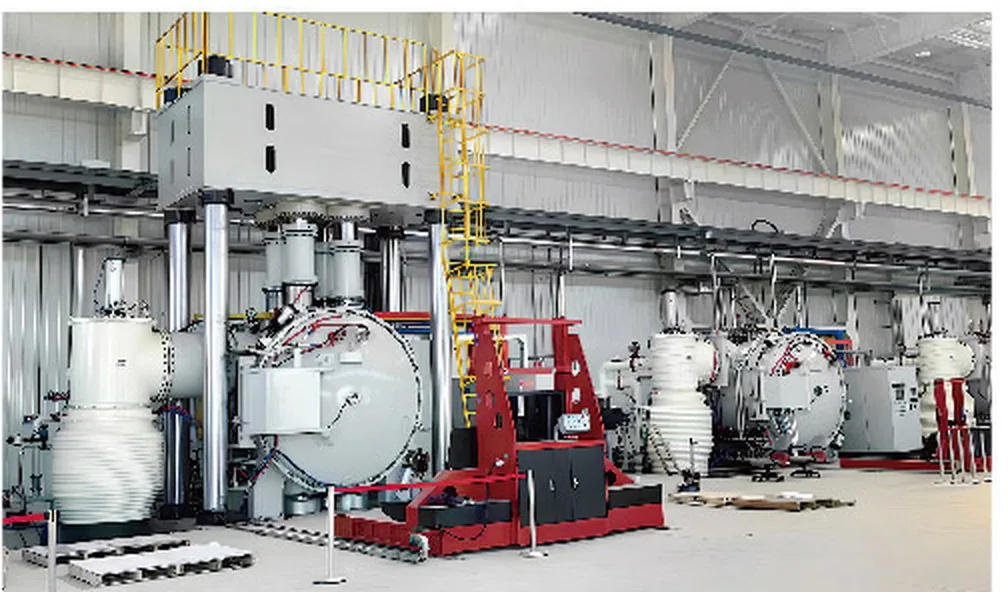
Wall thickness is only 0.5 mm with a 320 mm brazing perimeter; the previous atmosphere-furnace route required straightening and de-oxidation.
With the JVHB-135 high-temperature vacuum brazing furnace, four independently controlled zones and pre-placed foil were used: 15 ℃/min ramp, dwell at 5×10⁻³ Pa, gap held at 0.05–0.1 mm by tooling.
Graphite/moly tooling carries 240 parts per charge; uniformity ±3 ℃. The furnace links to the plant MES, recording a traceable process curve for every batch.
Results
First-pass yield rose from 93.5% to 99.2%, straightening was eliminated, shift output grew 2.1× and energy use fell 18%.
 Export project
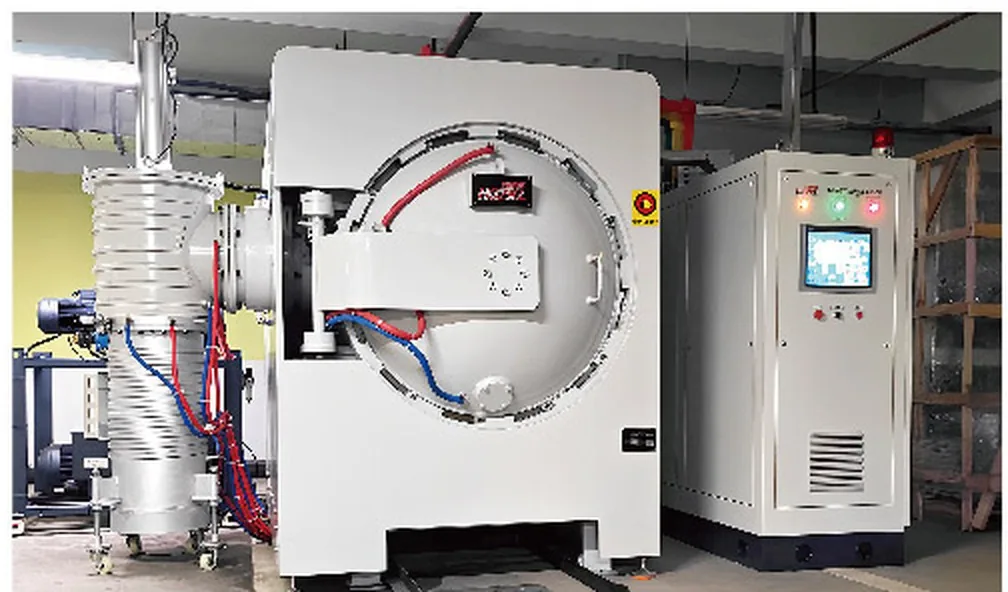
Vacuum diffusion bonding of titanium sandwich panels for spacecraft
800 mm sandwich parts retain 92% base-metal strength after bonding; leak rate 1×10⁻⁹ Pa·m³/s; three sets delivered, including export to Europe.
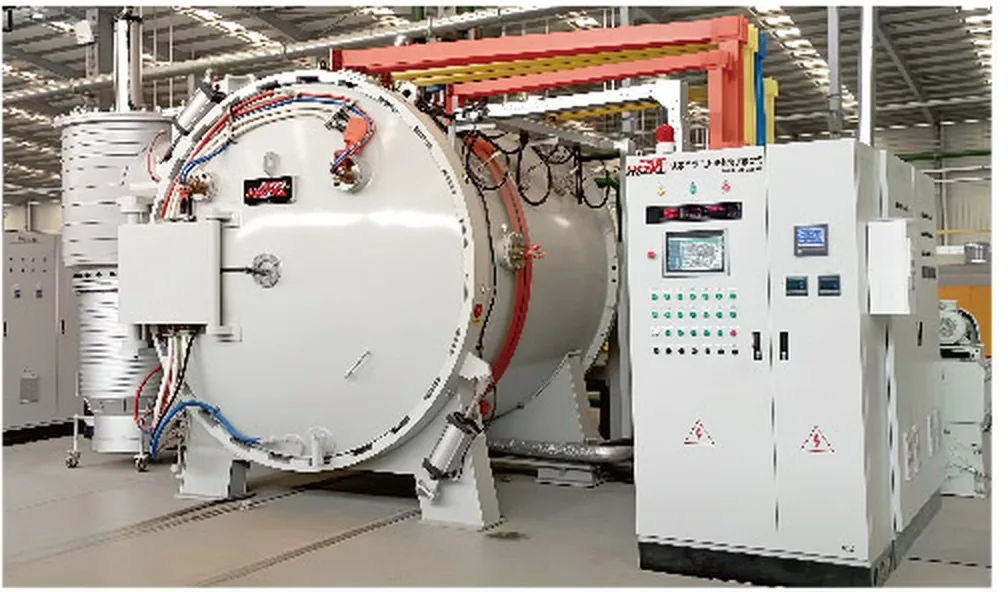
Distortion control of high-strength steel parts by high-pressure gas quench
18CrNiMo parts quenched in 10 bar nitrogen instead of oil: hardness HRC 48–51 across the charge, distortion down from 0.45 mm to 0.12 mm.
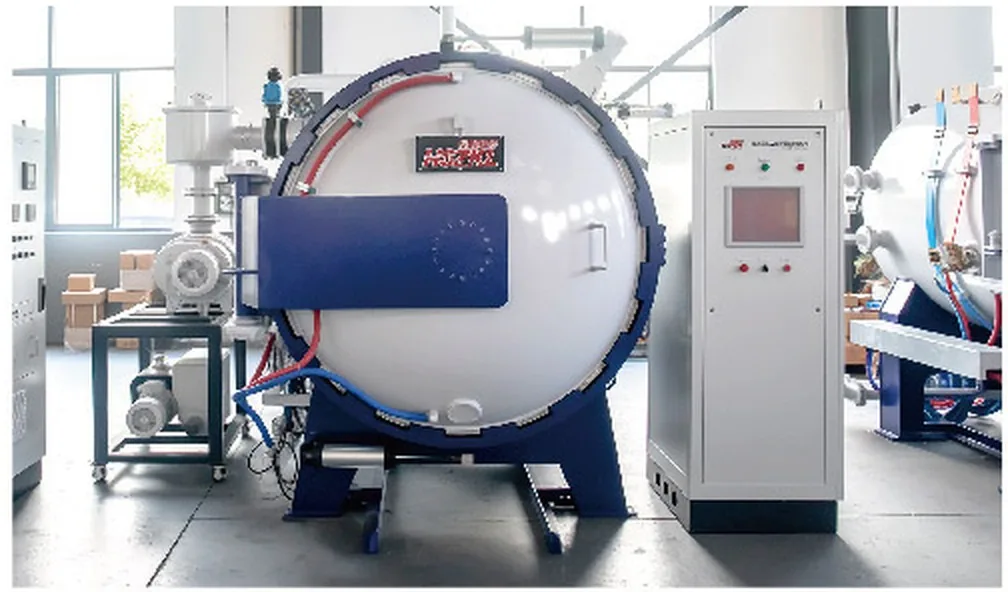
Two-chamber vacuum furnace line for transmission gears
Two chambers alternate heating and cooling on a 42-minute cycle, 1.6 t per day, linked to loading robots for unmanned operation.
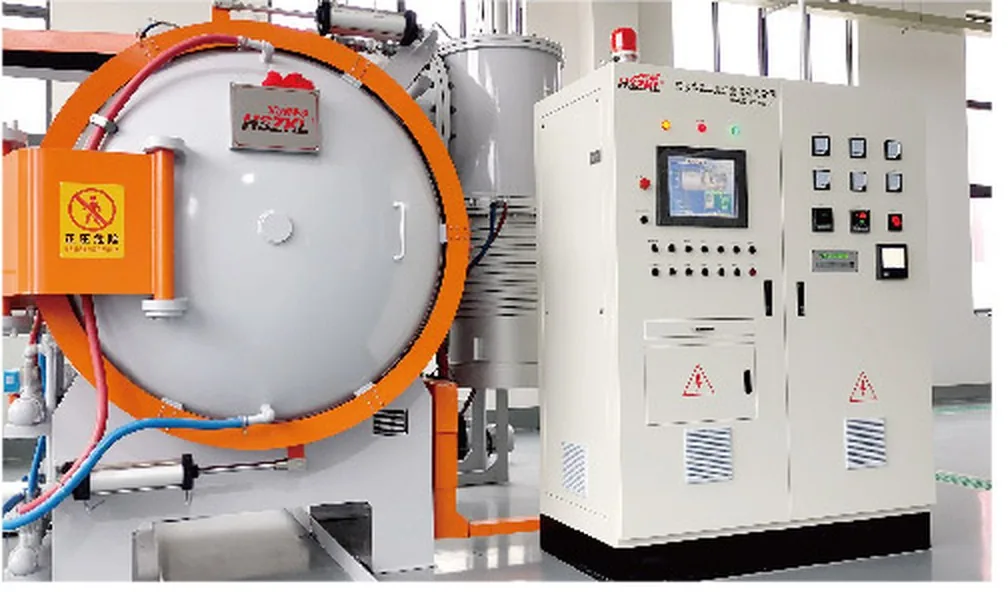 Export project
Export line for large cold-work tooling, vacuum oil quench
Cr12MoV blocks 180 mm thick, vacuum oil quenched with no scale or decarburisation, HRC 61–63; the furnace was exported with the tooling to Mexico.
Need a custom vacuum heat-treatment solution?
Send us the material, working zone and cycle time — we return a solution and a quote